 English
 العربية
 bosanski jezik
 Български
 Català
 粤语
 中文(漢字)
 Hrvatski
 Čeština
 Dansk
 Nederlands
 Eesti keel
 Suomi
 Français
 Deutsch
 Ελληνικά
 עברית
 Magyar
 Italiano
 日本語
 한국어
 Latviešu valoda
 Bahasa Melayu
 Norsk
 پارسی
 Polski
 Português
 Română
 Русский
 Cрпски језик
 Slovenčina
 Slovenščina
 Español
 Svenska
 தமிழ்
 ภาษาไทย
 Tiếng Việt

Βασικά σημεία σχεδιασμού καλωδίων σύνδεσης και ανάπτυξης παραγωγής
εγώ. Σχεδιασμός και ανάπτυξη
Διαδικασία σχεδιασμού
Ανάλυση απαιτήσεων: Διευκρινίστε τις ηλεκτρικές παραμέτρους (όπως ικανότητα μεταφοράς ρεύματος 400Α), φυσικό μέγεθος (η τελική πυκνότητα αυξήθηκε κατά 30%) και θέση εγκατάστασης της πλεξούδας, και προσαρμόστε τη σχεδίαση σε συνδυασμό με την αρχιτεκτονική του οχήματος (όπως ελεγκτής τομέα).
Αρθρωτός σχεδιασμός: Υιοθετήστε λύσεις πλατφόρμας (όπως το σύστημα μεγάλου βύσματος MX), ενσωματώστε τροφοδοτικό, λειτουργίες μετάδοσης σήματος και απαγωγής θερμότητας, Υποστηρίξτε τη λειτουργία hot plugging για να συντομεύσετε τον χρόνο αναβάθμισης OTA κατά 70%.
Έξοδος σχεδίασης: Σχεδιάστε ένα τρισδιάστατο διάγραμμα διάταξης μέσω επαγγελματικού λογισμικού, σημειώστε τις προδιαγραφές του καλωδίου, τύπους συνδετήρων και απαιτήσεις προστασίας, και ταυτόχρονα δημιουργούν έναν πίνακα βρόχων και ένα διάγραμμα κατεύθυνσης πλεξούδας.
Πρωτότυπα και Κατασκευή συναρμολόγησης προσαρμοσμένων καλωδίων
Key technology
Electromagnetic compatibility design: Use braided shielded wire and connectors with shielding layer to suppress electromagnetic interference (crosstalk is controlled below -50dB).
Layer or parallel arrangement of high and low voltage harnesses to reduce the interference of high voltage on low voltage system.
High-voltage system optimization:
The dual-track design ensures the stability of the DC high-voltage circuit. The connector must meet the requirements of high-voltage resistance (such as 48V system), high protection level and loop interlocking.
The dynamic voltage compensation algorithm controls the power supply fluctuation within ±0.5V to improve system reliability.
Schematic and Wiring Diagram Development:
Create detailed schematics and wiring diagrams to define component interactions and physical connections.
Component Selection:
Choose the appropriate wires, συνδετήρες, τερματικά, and insulation materials based on the requirements.
Harness Layout Design:
Plan the physical arrangement of wires, συνδετήρες, and other elements, considering space limitations, routing, and strain relief.
Πρωτοτυποποίηση:
Build a prototype to validate the design and make necessary adjustments before full-scale production.
2. Production and development
Core process
Raw material selection:
The wire uses high-temperature resistant copper core or aluminum core wire (such as high-voltage wire harness for new energy vehicles), and the connector needs to adapt to the terminal density and current requirements (such as DF53 series with 10A continuous current).
Το μονωτικό υλικό πρέπει να έχει επιβράδυνση φλόγας και αντίσταση ηλεκτρολυτών (όπως υποδοχή FPC της σειράς TB4).
Διαδικασία επεξεργασίας:
Κοπή σύρματος: Κόψτε σύμφωνα με την ακρίβεια σχεδίασης, και η ανοχή πρέπει να πληροί το πρότυπο υπολογισμού μήκους σύρματος.
Πρεσάρισμα ακροδεκτών: Χρησιμοποιήστε πλήρως αυτόματο εξοπλισμό πτύχωσης για να εξασφαλίσετε αντίσταση επαφής <5mΩ.
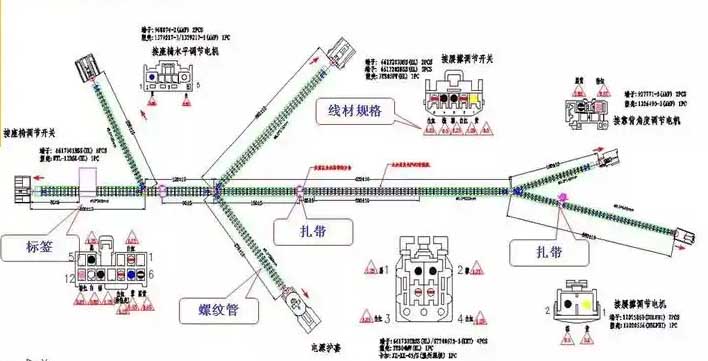
Προστασία συναρμολόγησης: Εισαγάγετε τον κυματοειδές σωλήνα ή τον εύκαμπτο σωλήνα, στερεώστε το με ένα δέσιμο καλωδίων, και προσθέστε ένα σήμα ετικέτας.

Ο αρθρωτός σχεδιασμός της πλεξούδας καλωδίωσης απλοποιεί την κατασκευή και τη συντήρηση
Επαλήθευση ποιότητας
Ηλεκτρική δοκιμή:
Δοκιμή συνέχειας για έλεγχο για ανοιχτό κύκλωμα, δοκιμή αντίστασης μόνωσης για ανίχνευση διαρροής, και να αντέχουν σε δοκιμή τάσης για να επαληθεύσουν τη σταθερότητα σε περιβάλλον υψηλής τάσης.
Δοκιμή ποσοστού σφάλματος bit (όπως διατηρεί η σειρά IT14 0.01% bit error rate at 85°C) ensures the reliability of high-speed signal transmission.
Mechanical and Environmental Test:
Δόνηση, salt spray and high and low temperature cycle tests to ensure the durability of the wiring harness under extreme working conditions.
Appearance inspection shows no burrs or damage, and the protective material is fully covered.
III. Industry Trends
Intelligent Integration: Through the fusion of sensors (such as RNC road noise sensors) and algorithms, noise reduction accuracy of ±0.5dB is achieved, and energy efficiency is optimized.
Lightweight and Efficient: Modular design reduces solder joints and wiring harness length (such as TB4 series reduces assembly hours by 70%), helping to reduce the weight of the vehicle by 12kg.
The above processes and technological innovations have been verified in mass production projects of companies such as Molex and Hirose Electric, covering new energy vehicles, κέντρα δεδομένων, and humanoid robots.
Η ανάπτυξη μιας πλεξούδας σύνδεσης περιλαμβάνει μια διαδικασία πολλαπλών σταδίων από το σχεδιασμό έως την παραγωγή. Ξεκινά με τον καθορισμό απαιτήσεων, δημιουργώντας ένα σχηματικό, επιλογή εξαρτημάτων, και στη συνέχεια απλώνοντας σωματικά το λουρί. Η παραγωγή περιλαμβάνει κοπή, απότομος, καλώδια σύνδεσης, συναρμολόγηση, και δοκιμή του τελικού προϊόντος.
The final plan for designing the connection harness is determined:
Concept: Before mass production of connected wire harnesses, process engineers need to verify the process method after dividing the work stations (ήτοι, the process method used during SOP). Adjustments and re-verifications are made during the verification process, and the finalized process method is the final plan.
Time to determine the plan: In the later stages of the PPAP stage, before the official ramp-up, process engineers need to finalize the final plan.
Determine the purpose of the program
1. In order to ensure the smooth progress of the process during the official launch. Problems discovered during the verification process can be solved as early as possible and will not be left during mass production.
2. There will be no major problems or bottleneck stations in the early stages of mass production.
3. It enables the team to complete mass production within the specified time, smoothly enter the SOP stage, and seamlessly connect with the customer’s SOP stage.
4. Ensure that the quality of the wire harness produced in the mass production stage is intact.
Custom Industrial & Medical Control Harnesses
Criteria for determining the final design of the connection harness
ΕΝΑ. Each station runs smoothly according to the process method. The so-called smoothness means that the process method operates smoothly, and people and people and machines cooperate with each other tacitly, without conflicts or waiting. The specific standards are as follows:
Correct assembly sequence
For the assembly of the wire harness assembly, the manual steps are complicated. When formulating the process method, special attention should be paid to the assembly sequence. Although the assembly sequence has been initially verified when accepting the operation card, when the final plan is determined, the content and sequence of the assembly still need to be studied and analyzed, because these work contents need to be completed within the cycle time. At this stage, more attention is paid to the details of the operator’s operations on the workstation, such as whether the material taken is in accordance with the operating sequence, whether there are conflicts in the operations of multiple people on the workstation, και τα λοιπά.
σι. The time for each station to complete the wire harness assembly is within the cycle. We require that the effective (value-added) operation time of each workstation not only needs to be within the cycle time, but also needs to be infinitely close to the cycle time, so as to ensure that the operator’s efficiency is maximized. Maximizing efficiency means maximizing the effective (value-added) operation time of personnel within the specified time. The concept involves effective, value-added operation time, which is specifically understood as follows:
For the operations in the wire harness production process, it is divided into the following four types:
1. Value-added actions: effective operations, operations necessary for wire harness production, such as inserting terminals, wrapping tape, and installing positioning parts. These are necessary actions when assembling components. Without these operations, the wiring harness cannot be assembled.
2. Actions that do not add value: Ήτοι, invalid operations, unnecessary operations for wire harness production. Such as straightening out the wires to prevent them from being disordered; holding the terminals in the wrong direction when inserting terminals; needing to rotate the wires to adjust the direction of the terminals, picking up dropped materials, και τα λοιπά. These actions are additional actions generated during assembly and will affect the assembly time. These actions are actions that IE needs to discover and eliminate.
3. Waiting: ήτοι, waiting within the specified time. There are two types of waiting: one is when the employee has completed all the work at this station, but the takt time has not yet reached and there is nothing to do, indicating that the workload at this station is not enough. The other is that employees need the line passed from the previous work station to complete the operation of this work station. Ωστόσο, at the specified time, the previous work station did not pass the incoming line, indicating that there was a bottleneck at the previous work station and the work could not be completed within the specified time and transferred to the next work station. These waits are also what IE needs to eliminate.
Walk back and forth:
When employees operate, they need to move from point A to point B before they can enter the operation; ωστόσο, there is no operation during the overshoot from A to B, only walking. The most common situation is that one employee operates two workstations, and the employee needs to go from A to B. These times of moving around are also undesirable. Επομένως, when laying out the workstation, try to put the content that the same employee needs to operate on one workstation, or place the workstation parts as close as possible to avoid moving back and forth.
We hope to fully schedule employees’ value-added operations within a limited cycle time and verify that it is feasible during the finalization of the solution.
ντο. The connection between workstations is clear and smooth. Specifically reflected in the following aspects:
1. When wire harnesses are transferred between workstations, the tools used for transfer are reasonably designed to make it easier for employees to place the wire harnesses. The wire harness is placed on the transfer tool in a clear manner without damaging the wire harness, and the quantity placed is clearly defined.
2. The transfer process is simple and easy for employees to operate. Συγχρόνως, it is easy to pick up the wiring harness at the next workstation.
3. The information is transmitted completely without loss. After getting the wire harness at this station, clearly guide the model or ID of the wire harness in hand. In testing the wiring harness, you need to use the wiring harness ID to retrieve the corresponding wiring harness program. Επομένως, during the delivery process, the carrier that displays the harness ID, such as the harness order or label, πρέπει να είναι συνεπής με την ίδια την ζώνη, και η ταυτότητα δεν μπορεί να χαθεί κατά την παράδοση.
Διαδικασία παραγωγής καλωδίων σύνδεσης
ΕΝΑ. Προπαρασκευαστικές εργασίες: Απαιτούνται κάποιες προκαταρκτικές προετοιμασίες πριν καθοριστεί το τελικό σχέδιο. Αυτές οι εργασίες πρέπει να προετοιμαστούν εκ των προτέρων πριν μπορέσει να εφαρμοστεί η επαλήθευση των μεθόδων διαδικασίας. Οι συγκεκριμένες λεπτομέρειες έχουν ως εξής:
1. Η κατάσταση εργαλείων και εξοπλισμού είναι ενημερωμένη και έχει κυκλοφορήσει. Επειδή οι αλλαγές μηχανικής πλεξούδας καλωδίωσης είναι συχνές, Οι μηχανικές αλλαγές είναι αναπόφευκτες ακόμη και κατά τη φάση της αναβάθμισης. Επομένως, τα εργαλεία και ο εξοπλισμός επιτόπου πρέπει να διασφαλίζουν ότι οι αλλαγές μηχανικής έχουν εφαρμοστεί σωστά και έχουν γίνει αποδεκτές από το τμήμα ποιότητας και μπορούν να χρησιμοποιηθούν για την παραγωγή.
2. Η διάταξη του χώρου παραγωγής είναι πλήρης και δεν υπάρχουν ελαττώματα. Η σχάρα εργαλείων τοποθετείται στη σωστή θέση, τα εργαλεία και ο εξοπλισμός είναι άθικτα και χωρίς σφάλματα, και τα εργαλεία που χρησιμοποιούνται τοποθετούνται στη σωστή θέση.
3. Η μέθοδος διαδικασίας έχει αρχικά επαληθευτεί από την IE, και η μηχανολογική κατάσταση είναι η πιο πρόσφατη.
4. Η κατάσταση των παραμέτρων που απαιτούνται για διάφορες παραγωγές είναι ενημερωμένη και έχει επαληθευτεί και κυκλοφορήσει.
5. Τα σύρματα και άλλες πρώτες ύλες πρέπει να μεταφέρονται με τον σωστό τρόπο (αγωγοί, κουτιά υλικών, και τα λοιπά.) και τοποθετείται στη σωστή θέση στη σχάρα εργαλείων.
6. Το σύστημα σύνδεσης έχει ολοκληρωθεί: τα εργαλεία σύνδεσης που χρησιμοποιούνται είναι λογικά σχεδιασμένα, η μετάδοση πληροφοριών είναι συνεχής και πλήρης, και τους φορείς πληροφοριών (παραγγελίες καλωδίων, κάρτες πληροφοριών, ετικέτες) used at the starting end of the information are all ready.
7. The network connection is good: test result recording and communication, wire harness tracking system, και τα λοιπά. are running normally, label printing is normal and the information displayed on the label is correct.
8. Operators are in place. Operators are required to be experience production employees. It requires employees with rich production experience, or employees with experience in the production of this wire harness, who are familiar with the assembly process of this wire harness and are skilled in operation. When multiple employees operate at the same work station, the number of employees on this work station needs to be matched and verified at the same time. Αλλιώς, it cannot be verified whether there is a conflict between workstations.
According to the process card, the operation content of each workstation is divided into several action units and placed in the action list. When dividing, you need to pay attention to the appropriate size of the action division. Γενικά, IE is measured manually on site with a stopwatch, and there are errors in the measurement itself. If the division is too fine, the errors present in the measurement will be amplified, resulting in inaccurate work hours for this action. If the division is too rough, the actual working hours of this action after some actions are moved to other stations cannot be obtained when balancing the work station. According to experience, this division method is generally followed:
1: Take the wires from the material rack, insert the terminals, and lay the wires (Αυτές οι τρεις ενέργειες σχηματίζουν γενικά μια μονάδα δράσης για μέτρηση).
2: Πάρτε τα πλαστικά μέρη από τη σχάρα υλικού και τοποθετήστε τα στο σταθερό εξάρτημα.
3: Το κύκλωμα στον ίδιο σταθμό εργασίας και στο ίδιο πλαστικό μέρος χωρίζεται σε πολλές μονάδες δράσης για δοκιμή. Μια μονάδα δράσης περιέχει περισσότερα από 2 βρόχους.
4: Πάρτε την ταινία από το ράφι υλικού, κόψτε την ταινία, και τυλίξτε το κλαδί. Γενικά, υπάρχει μία μονάδα δράσης ανά κλάδο.
5: Πάρτε το τεμάχιο τοποθέτησης από το ράφι υλικού, τοποθετήστε το τεμάχιο τοποθέτησης, και έκοψε την ουρά.
Μέτρηση ανθρωποωρών για την παραγωγή ιμάντων σύνδεσης:
Αφού ολοκληρωθούν οι προπαρασκευαστικές εργασίες, Ο IE πρέπει να μελετήσει κάθε σταθμό εργασίας και να μετρήσει τις ώρες λειτουργίας του. Οι συγκεκριμένες μέθοδοι υλοποίησης είναι οι εξής:
Πραγματικές ώρες εργασίας:
Μετά τη διαίρεση των μονάδων δράσης, fill in the working hours measurement table, and then measure the working hours according to the actions. 10 valid data need to be recorded. Judgment of valid data
in principle:
When the operation time of the unit is ≤30 seconds, the range of 10 sets of data should be: 90% * Average (10 sets of data) ~ 110% * Average (10 sets of data).
When the operation time of the unit is >30 δευτερόλεπτα, the range of 10 sets of data should be: 95%*Average (10 sets of data) ~ 105%*Average (10 sets of data).
Time spent walking around and waiting needs to be measured as well. In addition to recording actual operating hours, it is also necessary to observe the details of employees while operating. When measuring work hours, you need to distinguish between value-added and non-value-added actions. If it is found that there are non-value-added actions in the operation, the measured working hours need to be specially marked, and the test will be retested after improvement.
Σταθμός εξισορρόπησης για την παραγωγή ιμάντων σύνδεσης:
Οι ώρες εργασίας κάθε σταθμού εργασίας προστίθενται και εξάγονται για να σχηματιστεί ένας τοίχος ισορροπίας σταθμού εργασίας. Αναλύστε και ρυθμίστε τον τοίχο ισορροπίας του σταθμού εργασίας:
ένα. Εξάλειψη των σταθμών συμφόρησης: Μετακινήστε την εργασία που υπερβαίνει το χρόνο κύκλου σε σταθμό που δεν είναι γεμάτος. Όπως φαίνεται στην παρακάτω εικόνα, μέρος της εργασίας στο σταθμό 3 έχει μεταφερθεί στο σταθμό 2.
σι. Εξαλείψτε το χρόνο περπατήματος: παρατηρήστε την πραγματική λειτουργία και τοποθετήστε τα μέρη που πρέπει να μετακινηθούν μαζί όσο το δυνατόν περισσότερο
ντο. Εξάλειψη του χρόνου αναμονής: μετακινήστε την εργασία υπερχείλισης από άλλους σταθμούς σε αυτόν τον σταθμό
ρε. Ανακαλύψτε εργασία χωρίς προστιθέμενη αξία, βελτιστοποίηση σταθμών εργασίας, αύξηση του περιεχομένου εργασίας προστιθέμενης αξίας, και βελτίωση της αποτελεσματικότητας
-Μετά την εξισορρόπηση του σταθμού εργασίας
Μετά τη λήψη του νέου περιεχομένου εργασίας του σταθμού εργασίας, it is necessary to re-measure the working hours of the work station to verify whether the balanced solution is feasible. If there is still an imbalance after verification, the above operation needs to be repeated again.
ντο. Update process: After the work station is balanced, the content that needs to be updated is as follows: Determine the specific update items according to the actual situation.
1. Update the process operation card and resubmit it to quality release.
2. Update the workstation balance wall
3. Update the content of the tooling board, especially the content of the kit board and assembly line assembly board; quality release is still required after the update.
4. Update the content of equipment operation, parameter adjustment, και τα λοιπά., and submit it to quality release after updating.
5. Update the tool rack to include tools for connecting the system. Due to the adjustment of the workload, the corresponding materials used will also be adjusted. The corresponding tooling racks will take increasing and decreasing positions to place the materials, and the labels of the materials will be updated at the same time.
6. Update information flow, wire harness orders/labels and other information to be corrected based on the latest workstation information
7. Update the work layout on site, implement the latest design plan, and release quality again.
8. Train on-site operators according to the latest production process plan to familiarize them with the methods.