 English
 العربية
 bosanski jezik
 Български
 Català
 粤语
 中文(漢字)
 Hrvatski
 Čeština
 Dansk
 Nederlands
 Eesti keel
 Suomi
 Français
 Deutsch
 Ελληνικά
 עברית
 Magyar
 Italiano
 日本語
 한국어
 Latviešu valoda
 Bahasa Melayu
 Norsk
 پارسی
 Polski
 Português
 Română
 Русский
 Cрпски језик
 Slovenčina
 Slovenščina
 Español
 Svenska
 தமிழ்
 ภาษาไทย
 Tiếng Việt


Кључне тачке пројектовања и развоја производње прикључних свежња
Ја. Дизајн и развој
Процес дизајна
Анализа захтева: Појасните електричне параметре (као што је носивост струје 400А), физичка величина (терминална густина повећана за 30%) и место уградње појаса, и прилагодите дизајн у комбинацији са архитектуром возила (као што је контролер домена).
Модуларни дизајн: Усвојите платформска решења (као што је МКС систем великих конектора), интегрисати напајање, функције преноса сигнала и одвођења топлоте, подржавају хот плуггинг да скрате време ОТА надоградње 70%.
Излаз цртежа: Нацртајте тродимензионални дијаграм распореда помоћу професионалног софтвера, означите спецификације жице, типови конектора и захтеви заштите, и истовремено генерише табелу петље и дијаграм правца појаса.
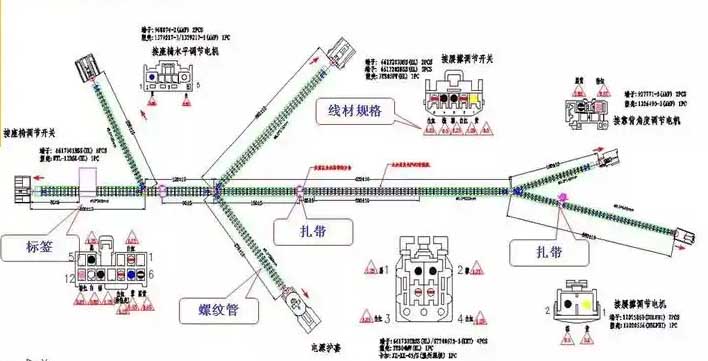
Прототипови и производња прилагођених жичара
Кључна технологија
Дизајн електромагнетне компатибилности: Користите плетену заштићену жицу и конекторе са заштитним слојем да бисте сузбили електромагнетне сметње (преслушавање се контролише испод -50дБ).
Слојевити или паралелни распоред каблова високог и ниског напона за смањење сметњи високог напона на нисконапонском систему.
Оптимизација високонапонског система:
Двоструки дизајн обезбеђује стабилност високонапонског кола једносмерне струје. Конектор мора испуњавати захтеве високонапонског отпора (као што је систем од 48 В), висок ниво заштите и преклапање петље.
Алгоритам динамичке компензације напона контролише флуктуацију напајања унутар ±0,5В да би побољшао поузданост система.
Израда шеме и дијаграма ожичења:
Направите детаљне шеме и дијаграме ожичења да бисте дефинисали интеракције компоненти и физичке везе.
Избор компоненти:
Изаберите одговарајуће жице, конектори, терминали, и изолационих материјала на основу захтева.
Дизајн распореда појаса:
Plan the physical arrangement of wires, конектори, и други елементи, considering space limitations, рутирање, и ослобађање од напрезања.
Израда прототипа:
Направите прототип да бисте потврдили дизајн и извршили неопходна подешавања пре пуне производње.
2. Production and development
Основни процес
Raw material selection:
Жица користи бакарну или алуминијумску жицу отпорну на високе температуре (као што је сноп високонапонских жица за возила нове енергије), а конектор треба да се прилагоди густини прикључака и захтевима струје (such as DF53 series with 10A continuous current).
The insulating material must have flame retardancy and electrolyte resistance (such as TB4 series FPC connector).
Processing process:
Wire cutting: Cut according to the drawing precision, and the tolerance must meet the wire length calculation standard.
Terminal crimping: Use fully automatic crimping equipment to ensure contact resistance <5мΩ.
Assembly protection: Insert the corrugated tube or hose, fix it with a cable tie, and add a label mark.

Modular wiring harness design simplifies manufacturing and maintenance
Quality Verification
Electrical Test:
Continuity test to check for open circuit, insulation resistance test to detect leakage, and withstand voltage test to verify stability in high-voltage environment.
Bit error rate test (such as IT14 series maintains 0.01% брзина битне грешке на 85°Ц) обезбеђује поузданост преноса сигнала велике брзине.
Механички и еколошки тест:
Вибрација, слани спреј и тестови циклуса на високим и ниским температурама како би се осигурала издржљивост снопа ожичења у екстремним радним условима.
Преглед изгледа не показује избочине или оштећења, а заштитни материјал је у потпуности покривен.
Иии. Индустри Трендс
Интелигентна интеграција: Кроз фузију сензора (као што су РНЦ сензори буке на путу) и алгоритми, постиже се тачност смањења шума од ±0,5дБ, а енергетска ефикасност је оптимизована.
Лаган и ефикасан: Модуларни дизајн смањује лемне спојеве и дужину кабелског свежња (као што је серија ТБ4 смањује сате монтаже за 70%), помаже да се тежина возила смањи за 12 кг.
The above processes and technological innovations have been verified in mass production projects of companies such as Molex and Hirose Electric, covering new energy vehicles, data centers, and humanoid robots.
Развијање везнем свежња укључује више факултету од дизајна до производње. Почиње са дефинисањем захтева, Стварање шеме, Одабир компоненти, а затим физички положити појас. Производња укључује сечење, скидање, Повезивање жица, састављање, и тестирање готовог производа.
The final plan for designing the connection harness is determined:
Concept: Before mass production of connected wire harnesses, process engineers need to verify the process method after dividing the work stations (то је, the process method used during SOP). Adjustments and re-verifications are made during the verification process, and the finalized process method is the final plan.
Time to determine the plan: In the later stages of the PPAP stage, before the official ramp-up, process engineers need to finalize the final plan.
Determine the purpose of the program
1. In order to ensure the smooth progress of the process during the official launch. Problems discovered during the verification process can be solved as early as possible and will not be left during mass production.
2. There will be no major problems or bottleneck stations in the early stages of mass production.
3. It enables the team to complete mass production within the specified time, smoothly enter the SOP stage, and seamlessly connect with the customer’s SOP stage.
4. Ensure that the quality of the wire harness produced in the mass production stage is intact.
Custom Industrial & Medical Control Harnesses
Criteria for determining the final design of the connection harness
А. Each station runs smoothly according to the process method. The so-called smoothness means that the process method operates smoothly, and people and people and machines cooperate with each other tacitly, without conflicts or waiting. The specific standards are as follows:
Correct assembly sequence
For the assembly of the wire harness assembly, the manual steps are complicated. When formulating the process method, special attention should be paid to the assembly sequence. Although the assembly sequence has been initially verified when accepting the operation card, when the final plan is determined, the content and sequence of the assembly still need to be studied and analyzed, because these work contents need to be completed within the cycle time. At this stage, more attention is paid to the details of the operator’s operations on the workstation, such as whether the material taken is in accordance with the operating sequence, whether there are conflicts in the operations of multiple people on the workstation, итд.
Б. The time for each station to complete the wire harness assembly is within the cycle. We require that the effective (value-added) operation time of each workstation not only needs to be within the cycle time, but also needs to be infinitely close to the cycle time, so as to ensure that the operator’s efficiency is maximized. Maximizing efficiency means maximizing the effective (value-added) operation time of personnel within the specified time. The concept involves effective, value-added operation time, which is specifically understood as follows:
For the operations in the wire harness production process, it is divided into the following four types:
1. Value-added actions: effective operations, operations necessary for wire harness production, such as inserting terminals, wrapping tape, and installing positioning parts. These are necessary actions when assembling components. Without these operations, the wiring harness cannot be assembled.
2. Actions that do not add value: То је, invalid operations, unnecessary operations for wire harness production. Such as straightening out the wires to prevent them from being disordered; holding the terminals in the wrong direction when inserting terminals; needing to rotate the wires to adjust the direction of the terminals, picking up dropped materials, итд. These actions are additional actions generated during assembly and will affect the assembly time. These actions are actions that IE needs to discover and eliminate.
3. Waiting: то је, waiting within the specified time. There are two types of waiting: један је када је запослени завршио све послове на овој станици, али време текта још није стигло и нема шта да се ради, што указује да оптерећење на овој станици није довољно. Други је да је запосленима потребна линија која је прошла са претходне радне станице да би завршили рад ове радне станице. Међутим, у назначено време, претходна радна станица није прошла долазну линију, указујући да је на претходној радној станици било уско грло и да се посао није могао завршити у наведеном року и пренети на следећу радну станицу. Ова чекања су такође оно што ИЕ треба да елиминише.
Ходајте напред-назад:
Када запослени раде, потребно је да се преселе од тачке А до тачке Б пре него што уђу у операцију; међутим, нема операције током прекорачења од А до Б, само ходање. Најчешћа ситуација је да један запослени ради са две радне станице, а запослени треба да иде од А до Б. Ова времена кретања су такође непожељна. Стога, при постављању радне станице, покушајте да садржај који је истом запосленом потребан за рад поставите на једну радну станицу, или поставите делове радне станице што ближе како бисте избегли померање напред-назад.
Надамо се да ћемо у потпуности заказати операције са додатом вредношћу запослених у оквиру ограниченог времена циклуса и проверити да ли је то изводљиво током финализације решења.
Ц. Веза између радних станица је јасна и глатка. Посебно се огледа у следећим аспектима:
1. Када се каблови преносе између радних станица, the tools used for transfer are reasonably designed to make it easier for employees to place the wire harnesses. The wire harness is placed on the transfer tool in a clear manner without damaging the wire harness, and the quantity placed is clearly defined.
2. The transfer process is simple and easy for employees to operate. У исто време, it is easy to pick up the wiring harness at the next workstation.
3. The information is transmitted completely without loss. After getting the wire harness at this station, clearly guide the model or ID of the wire harness in hand. In testing the wiring harness, you need to use the wiring harness ID to retrieve the corresponding wiring harness program. Стога, during the delivery process, the carrier that displays the harness ID, such as the harness order or label, must be consistent with the harness itself, and the identity cannot be lost during delivery.
Connection harness production process
А. Preparatory work: Some preliminary preparations are required before the final plan is determined. These tasks need to be prepared in advance before the verification of process methods can be implemented. The specific details are as follows:
1. The tooling and equipment status is up to date and has been released. Because wiring harness engineering changes are frequent, engineering changes are inevitable even during the ramp-up phase. Стога, the on-site tooling and equipment need to ensure that the engineering changes have been implemented correctly and have been accepted by the quality department and can be used for production.
2. The layout of the on-site production area is complete and there are no defects. The tool rack is placed in the correct position, the tooling and equipment are intact and fault-free, and the tools used are placed in the correct position.
3. The process method has been initially verified by IE, and the engineering status is the latest.
4. The status of parameters required for various productions is up to date and has been verified and released.
5. Wires and other raw materials should be carried in the correct way (проводници, material boxes, итд.) and placed in the correct position on the tooling rack.
6. The connection system is complete: the connection tools used are reasonably designed, the information transmission is continuous and complete, and the information carriers (wire harness orders, information cards, labels) које се користе на почетном крају информација су све спремне.
7. Мрежна веза је добра: снимање резултата теста и комуникација, систем за праћење каблова, итд. раде нормално, штампање етикете је нормално и информације приказане на етикети су тачне.
8. Оператери су на месту. Од оператера се захтева да буду запослени у производњи. Захтева запослене са богатим производним искуством, или запослени са искуством у производњи овог жичаног појаса, који су упознати са процесом монтаже овог снопа и вешти у руковању. Када више запослених ради на истој радној станици, број запослених на овој радној станици треба да се упореди и верификује истовремено. Иначе, не може се проверити да ли постоји конфликт између радних станица.
According to the process card, the operation content of each workstation is divided into several action units and placed in the action list. When dividing, you need to pay attention to the appropriate size of the action division. Генерално, IE is measured manually on site with a stopwatch, and there are errors in the measurement itself. If the division is too fine, the errors present in the measurement will be amplified, resulting in inaccurate work hours for this action. If the division is too rough, the actual working hours of this action after some actions are moved to other stations cannot be obtained when balancing the work station. According to experience, this division method is generally followed:
1: Take the wires from the material rack, insert the terminals, and lay the wires (these three actions generally form an action unit for measurement).
2: Take the plastic parts from the material rack and place them in the fixed fixture.
3: The circuit in the same work station and the same plastic part is divided into several action units for testing. An action unit contains more than 2 loops.
4: Take the tape from the material rack, tear off the tape, and wrap the branch. Генерално, there is one action unit per branch.
5: Take the positioning piece from the material rack, install the positioning piece, and cut off the tail.
Measurement of man-hours for producing connection harnesses:
After the preparatory work is completed, IE needs to study each workstation and measure its operating hours. The specific implementation methods are as follows:
Actual working hours:
After dividing the action units, fill in the working hours measurement table, and then measure the working hours according to the actions. 10 valid data need to be recorded. Judgment of valid data
in principle:
When the operation time of the unit is ≤30 seconds, the range of 10 sets of data should be: 90% * Average (10 sets of data) ~ 110% * Average (10 sets of data).
When the operation time of the unit is >30 секунди, the range of 10 sets of data should be: 95%*Average (10 sets of data) ~ 105%*Average (10 sets of data).
Time spent walking around and waiting needs to be measured as well. In addition to recording actual operating hours, it is also necessary to observe the details of employees while operating. When measuring work hours, you need to distinguish between value-added and non-value-added actions. If it is found that there are non-value-added actions in the operation, the measured working hours need to be specially marked, and the test will be retested after improvement.
Balancing station for producing connection harnesses:
The working hours of each workstation are added and extracted to form a workstation balance wall. Analyze and adjust the work station balance wall:
а. Eliminate bottleneck stations: Move work that exceeds the cycle time to a station that is not full. As shown in the picture below, part of the work in station 3 has been moved to station 2.
б. Eliminate walking time: observe the actual operation and put the parts that need to be moved together as much as possible
ц. Eliminate waiting time: move overflow work from other stations to this station
д. Discover non-value-added work, optimize work stations, increase value-added work content, and improve efficiency
-After balancing the workstation
After obtaining the new work content of the work station, it is necessary to re-measure the working hours of the work station to verify whether the balanced solution is feasible. If there is still an imbalance after verification, the above operation needs to be repeated again.
Ц. Update process: After the work station is balanced, the content that needs to be updated is as follows: Determine the specific update items according to the actual situation.
1. Update the process operation card and resubmit it to quality release.
2. Update the workstation balance wall
3. Update the content of the tooling board, especially the content of the kit board and assembly line assembly board; quality release is still required after the update.
4. Update the content of equipment operation, parameter adjustment, итд., and submit it to quality release after updating.
5. Update the tool rack to include tools for connecting the system. Due to the adjustment of the workload, the corresponding materials used will also be adjusted. The corresponding tooling racks will take increasing and decreasing positions to place the materials, and the labels of the materials will be updated at the same time.
6. Update information flow, wire harness orders/labels and other information to be corrected based on the latest workstation information
7. Update the work layout on site, implement the latest design plan, and release quality again.
8. Train on-site operators according to the latest production process plan to familiarize them with the methods.